How Do You Verify a Supplier Can Deliver a Complete Packaging Line?
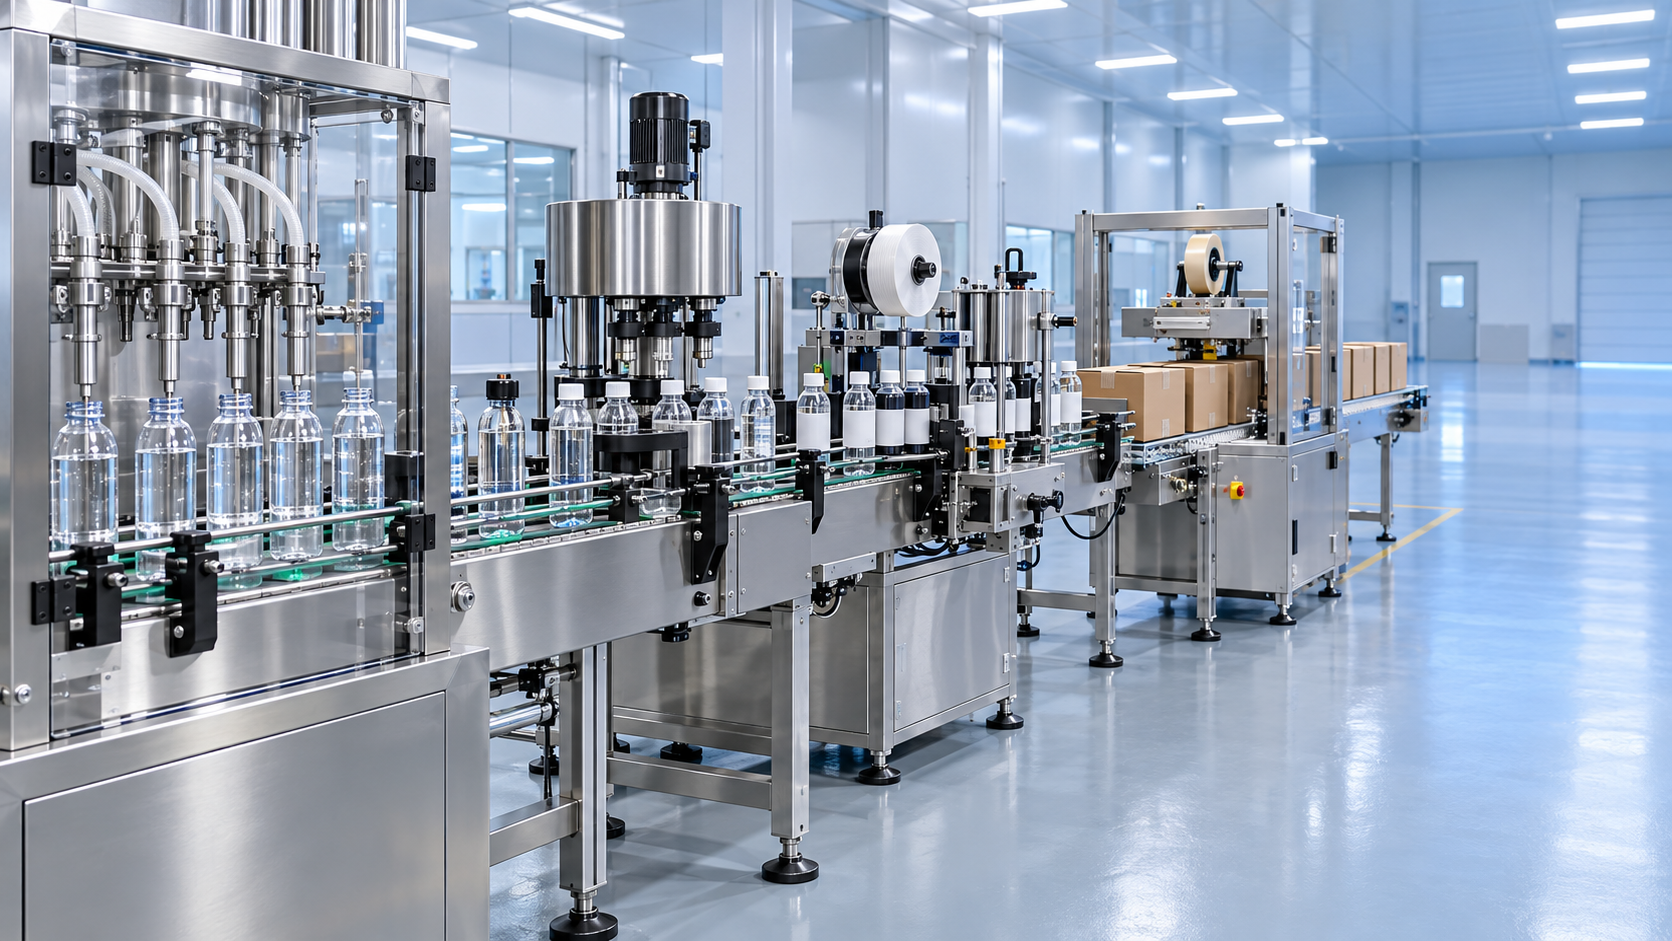
A supplier may offer every machine on your list, but can those machines work together as a complete packaging line? Before investing in filling equipment, verify more than catalog specifications. The real questions concern product compatibility, output under realistic conditions, responsibility for integration, and what happens when the line stops after installation.
A useful way to evaluate a proposal is to follow one bottle from entry to sealed carton. At every transfer, ask what controls its movement, what could interrupt production, and who must fix the problem. That exercise often reveals more than a long equipment list.
Define what “complete” means before comparing suppliers
“Complete packaging line” is not a sufficiently precise scope of supply. One quotation may include bottle rinsing, automatic filling, capping, conveying, and carton sealing. Another may stop at the capper discharge. Both can look comprehensive until you examine the exclusions.
Request a process flow diagram, a dimensioned layout, and an equipment schedule that identifies included equipment, optional items, and buyer-supplied services. Depending on the application, the process may also require filtration, bottle drying, shrink equipment, inspection, coding, labeling, or carton loading. A carton sealer, for example, does not automatically include equipment to erect or pack cartons.
The same clarification applies upstream. A filling machine needs a reliable product supply, but the quotation may exclude the feed tank, transfer pump, level controls, and connecting pipework. Ask where the supplier’s responsibility physically begins and ends.
For a small business, a semi-automatic packing station may be a sensible cost-saving choice. It is not a problem if that limitation is deliberate and included in the capacity calculation. It becomes a problem when “complete” conceals an unplanned manual operation.
Look for evidence of integration, not just machine manufacturing
Manufacturing a capable filler and delivering an integrated line are different tasks. The latter requires coordination across mechanical transfers, control signals, safety functions, product handling, and commissioning.
Ask for evidence from comparable applications. Relevant experience means similar product behavior, container stability, closure type, operating conditions, and automation level—not merely another project described as a beverage line.
- Request continuous running footage showing transfers between machines, rather than isolated demonstrations.
- Ask to review a redacted acceptance report or project document showing how performance was measured.
- Where permission allows, speak with a reference customer about commissioning, recurring stoppages, and service response.
- Ask which equipment the supplier manufactures, purchases, or integrates through an OEM partner.
Outsourced equipment is not automatically a weakness. A specialist capper or inspection system may be the right choice. The concern is divided accountability. If bottles jam between a purchased capper and the conveyor, one named party should own the investigation and correction—not send you between two manufacturers.
Make the supplier assess your actual product and packaging
A water trial can demonstrate basic machine operation. It cannot establish that the same configuration will handle foaming detergent, viscous edible oil, or juice containing pulp.
Provide representative product samples where practical, together with viscosity at operating temperature, foaming behavior, solids content, and relevant chemical compatibility information. Include actual bottles, caps or corks, labels, and cartons. Packaging drawings alone may not reveal how a lightweight bottle behaves under conveyor back pressure.
The supplier should explain the proposed filling method and its limitations. Detergent may require a filling sequence that controls foam. Oil can expose dripping and stringing problems at the nozzle. Soy sauce or vinegar requires assessment of wetted materials and seals. Wine handling may involve oxygen exposure and closure considerations. Filtration must suit the product; it should not unintentionally remove desired pulp or other ingredients.
Do not accept “food-grade” as a complete hygiene specification. Ask about product-contact materials, drainability, cleaning access, seal compatibility, and the intended cleaning procedure. Pharmaceutical applications may require additional documentation and qualification support, depending on the process and applicable requirements. A general-purpose liquid line is not automatically suitable.
Verify saleable output, not the filler’s headline speed
The number that matters is the quantity of acceptable finished packs produced over an agreed period. A filler’s maximum cycling rate does not tell you whether the cap feeder, shrink section, or packing station can keep up.
Ask the supplier to state expected line output for each important product and container combination. Larger fills, narrow bottle openings, unstable containers, and foaming products may change achievable performance. If one speed is quoted for every format, ask what assumptions support it.
Conveyor design deserves particular attention. Accumulation can absorb brief interruptions, but excessive back pressure can tip or deform bottles. The control system should coordinate upstream and downstream machines: stop feeding when a discharge is blocked, avoid filling without a container, and restart without creating a surge.
A revealing question is: “What happens if the carton sealer stops while the filler is running?” The answer should describe sensor logic, available accumulation, controlled stopping, and recovery—not simply promise that the conveyors are synchronized.
Write the acceptance test before placing the order
Factory acceptance testing, or FAT, is most useful when the protocol is agreed before manufacturing. Otherwise, the demonstration may prove only that individual machines move and fill.
Define the test product, packaging formats, run duration, sampling method, staffing, and pass criteria. Use representative materials wherever possible. If the actual product cannot be shipped, document what the substitute can demonstrate and which risks remain for site testing.
- Output: Count accepted finished packs over the agreed run, recording stops and their causes.
- Fill performance: Specify whether quantity is assessed by mass or volume, the tolerance, sampling frequency, and measurement method.
- Package quality: Check closure application, leakage, bottle damage, and downstream pack condition using agreed criteria.
- Fault recovery: Demonstrate blocked discharge, missing containers, interrupted feeds, and relevant safety functions under controlled conditions.
- Changeover: Change between agreed formats, including adjustment, cleaning where applicable, and production of acceptable packs.
Record manual interventions during the test. A line that runs only while technicians repeatedly straighten bottles or adjust sensors has not demonstrated stable automatic operation.
If the supplier cannot assemble the entire line before shipment, establish an alternative verification plan. Identify which interfaces will be tested separately, what remains unproven, and how unresolved integration work will be handled at your site. Acknowledge the added commissioning risk rather than treating separate machine tests as equivalent evidence.
Check whether the line will work in your building
A layout that fits inside the available floor area may still be impractical. Operators need access to refill closures, clear rejects, remove guards for authorized maintenance, clean equipment, and replace components. Tanks, electrical cabinets, and machine doors need usable clearance.
Confirm electrical supply, compressed-air quality and demand, water requirements, drainage, ventilation, and any process-specific utilities. Ask whether quoted consumption figures represent average use or peak demand. Shrink and drying equipment also needs assessment for heat management and compatibility with the containers and product.
Arrange a site review before the layout is frozen. Delivery access, floor conditions, utility connection points, and the route from unloading to final position should not be left for the installation crew to discover.
Site acceptance testing should then confirm operation with the installed utilities, upstream product supply, downstream handling, and your operators. FAT reduces uncertainty; it does not replace verification under actual production conditions.
Make support and responsibility contractual
“After-sales support available” is too vague to evaluate. Ask who attends commissioning, how training is delivered, what remote troubleshooting covers, and how on-site assistance is arranged. Separate a promised response time from the time required to restore production.
Request a recommended spare-parts list with part numbers, prices, availability, and replacement guidance. Pay particular attention to wear parts, sensors, proprietary change parts, and components sourced from third-party machines. Confirm access to electrical drawings, operating manuals, maintenance instructions, and control-system backups or recovery arrangements.
The contract should identify responsibility for installation, inter-machine wiring, software integration, training, and correcting failed acceptance items. Payment milestones can be linked to documented delivery and acceptance stages, subject to negotiated terms. Any deviations accepted during testing should have an owner and a completion date.
Choose the proposal with the fewest unresolved interfaces
A credible supplier does not need to promise unlimited flexibility. It should explain which products and formats the line can handle, where performance changes, and which upgrades require additional equipment. That matters especially for a tailored small-business line expected to expand later.
Before committing, ask for one coordinated package: the agreed scope, product and packaging specification, layout, performance commitments, acceptance protocol, and service responsibilities. Read those documents together. If a machine appears on the quotation but its transfer, control logic, or acceptance criteria are missing, the line is not yet fully defined.
The strongest evidence is not a full catalog. It is a supplier’s ability to show how your product reaches a finished carton—and to accept clear responsibility when any part of that process fails.
Thank you very much for writing to us. Please leave your message and contact information, we will reply to you within 24 hours.