How Should Suck-Back Be Adjusted to Stop Oil Filling Nozzle Drips?
How Should Suck-Back Be Adjusted to Stop Oil Filling Nozzle Drips?
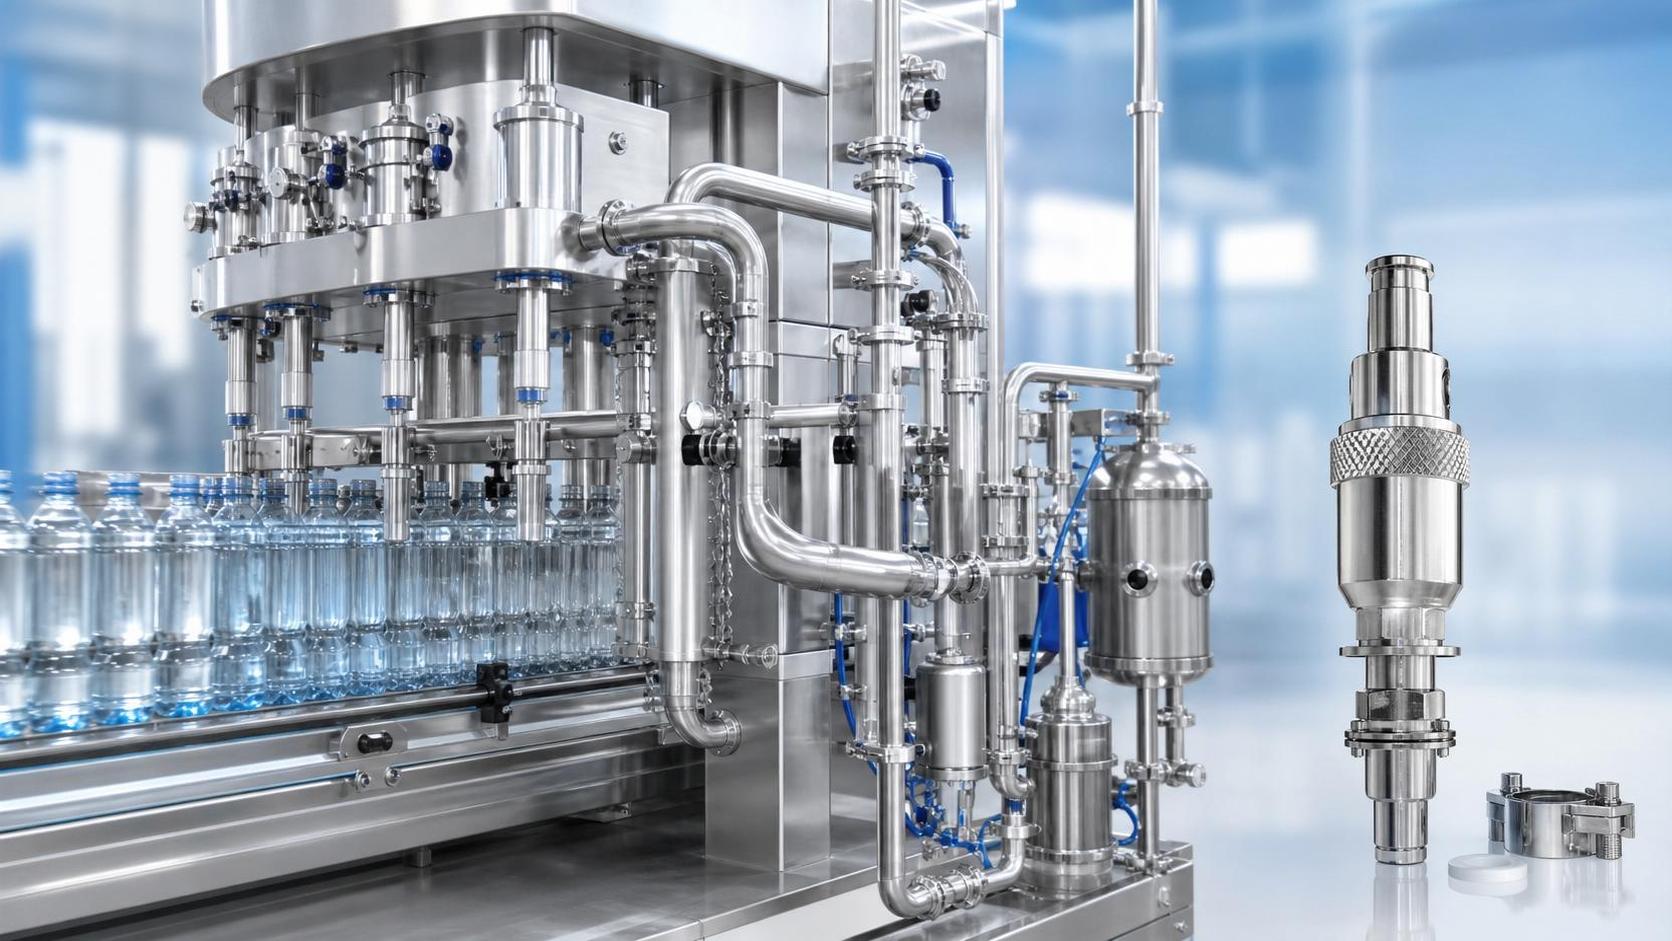
Oil dripping from filling nozzles can stain bottles, waste product, and create extra cleanup on your packaging line. If you need an effective oil filling nozzle dripping fix, start by checking suck-back—the controlled retraction that draws residual oil away from the nozzle tip after dispensing. Too little can leave drops hanging; too much may pull air into the product path and disrupt the next fill.
The practical target is not maximum suction. It is the smallest repeatable retraction that leaves the tip stable until the next bottle arrives, without disturbing fill accuracy. Getting there means checking what the nozzle actually does, then adjusting volume, speed, and timing separately where the machine allows it.
Watch when the drop forms before changing anything
Observe the end of a fill through the machine guarding, using a safe viewing position or video if needed. Does the drop form immediately at cutoff, develop while the nozzle rises, or appear only after the nozzle has waited above the conveyor? Those are different faults, even if they leave the same oily bottle shoulder.
A hanging drop immediately after dispensing can indicate insufficient retraction or oil remaining on the outside of the tip. A tip that initially clears but slowly becomes wet again suggests continued product feed, trapped pressure, or a leaking shutoff. A drop released during nozzle movement may be external oil shaken loose by acceleration.
Also compare heads. When every nozzle starts dripping after a recipe change, shared settings, oil temperature, or supply pressure deserve attention. When one head drips and the others remain clean, inspect that head before increasing suck-back across the machine.
Confirm what the suck-back setting actually controls
“Suck-back” is not one universal mechanism. A servo-driven positive-displacement filler may reverse its pump briefly. A piston system may use a dedicated retraction stroke or valve arrangement. An anti-drip nozzle may create local retraction as its internal mechanism closes. Other machines rely mainly on positive shutoff and offer little independent suction adjustment.
This distinction matters because a closed valve can isolate the nozzle tip from an upstream pump. Reversing that pump will not necessarily withdraw oil from the exposed outlet. Before experimenting with valve delays, check the manufacturer’s operating sequence and identify where retraction occurs relative to the shutoff seat.
An HMI value might represent reverse rotation, piston travel, time, or an arbitrary recipe unit—not milliliters. Record the original setting and its units. Do not assume a value from another filler, or even another nozzle size on the same machine, will produce equivalent retraction.
Tune retraction volume first, under steady conditions
Start with the correct oil, normal operating temperature, stable product supply, and clean nozzle tips. Prime the product path using the approved procedure. An air pocket left after cleaning can make an otherwise sensible setting look inconsistent.
Keep the main filling profile unchanged while you investigate the cutoff. If you alter final filling speed, retraction, nozzle height, and conveyor timing together, you may get a clean bottle without knowing which change worked—or why the next production run fails.
- Record the current recipe, product temperature, supply conditions, and which heads drip.
- Increase suck-back volume by the smallest practical increment permitted by the controls and manufacturer’s guidance.
- Run repeated fills and observe both the tip after cutoff and the start of the following fill. One clean cycle is not enough.
- Continue only while the additional retraction improves cutoff without creating bubbles, delayed flow, or unstable fill quantities.
- Once the tip stays clean, test whether a slightly lower setting also works. Retain the lowest stable setting and verify it at production speed.
Where the outlet is visible, the oil meniscus should retreat enough to stop a hanging drop from growing. It does not need to disappear far into the tube. Deep withdrawal creates more empty space to refill and can draw air through the outlet.
Check net fill by the line’s normal quality-control method during these trials. Depending on the metering arrangement, reverse movement may affect delivered quantity or the next cycle’s startup. Do not compensate for a drifting fill weight until you have established whether excessive retraction caused it.
The signs that you have gone too far
Watch for a brief sputter at the next start, visible air in a transparent product section, a delayed stream, or increased fill-to-fill variation. These symptoms are not proof of excessive suck-back—an inlet leak can also introduce air—but their appearance immediately after an adjustment is a useful clue.
Return to the previous stable setting before investigating further. More suction is not a sensible response to a problem that more suction just created.
Use speed and timing to clean up the cutoff
Once retraction volume is close, adjust speed if it is independently available. Thick oil may not follow a sharp reverse movement cleanly through a restrictive nozzle. A gentler retraction can be worth testing, provided it finishes within the available cycle time. An excessively slow movement, however, may allow the drop to detach before it is withdrawn.
Timing should follow the machine’s intended valve sequence. Retraction generally needs to act at the end of dispensing while it can still influence the residual oil at the outlet. Starting it too early can interrupt the final delivery; starting it too late may leave a drop falling outside the bottle.
On a diving-nozzle filler, examine retraction alongside nozzle lift. If the head rises while a liquid bridge still connects the tip to the oil surface, that bridge can stretch and break onto the bottle neck. A short dwell may help, but first confirm the permitted sequence. Do not simply slow the entire machine to conceal poor cutoff.
The order of adjustment matters: establish adequate volume, refine retraction speed, then check its relationship with valve closure and nozzle movement. If only one combined control exists, treat each change as a combined adjustment and document the result accordingly.
Account for oil temperature, pressure, and nozzle geometry
A setting developed during a cool startup may behave differently once the oil and filling circuit warm up. Many oils become less viscous as temperature rises, making them easier to dispense but also more likely to seep through a marginal valve seat. Colder oil may leave a persistent strand or respond sluggishly to retraction.
Record actual product temperature near the filling process rather than relying only on room temperature. For lines handling several edible oils, validate separate recipes where their behavior differs. A recipe used for soy sauce, juice, wine, or detergent should not be transferred to oil simply because the same filler can handle those products.
Supply conditions can be equally important. A changing tank level, unstable feed pump, or pressure-control problem may push oil back toward the tip after retraction. Flexible hoses can also store and release pressure. If the outlet clears and then refills, check these conditions instead of repeatedly increasing the reverse stroke.
Nozzle geometry affects the required setting. A wider outlet contains more liquid for the same length of withdrawal, while a narrow passage offers greater flow resistance. Product retained outside a scratched, burred, or poorly cleaned tip may not respond to internal suction at all. Avoid polishing or modifying nozzle surfaces without manufacturer approval.
Know when adjustment has reached its limit
Persistent dripping from one nozzle, especially when that head needs far more retraction than its neighbors, calls for inspection. Stop, isolate, depressurize, and follow the machine’s maintenance procedure before opening any product-contact assembly.
Check the shutoff seat, seals, closing mechanism, and tip for wear, deposits, or damage. Where pneumatic actuation is used, inconsistent air supply or sluggish valve movement can prevent repeatable closure. Also check for trapped particles; upstream filtration does not rule out debris introduced during maintenance or cleaning.
A useful distinction is whether oil merely remains at the tip or continues arriving there. Suck-back can manage a small residual volume. It cannot reliably overcome continuous leakage through a valve that should be closed. Increasing retraction to compensate may produce alternating drips and air ingestion without fixing either problem.
Validate the result on the complete packaging line
After tuning, test normal running, the first fills after a routine pause, and operation at the intended production rate. Inspect bottle necks, shoulders, and conveyor surfaces—not just the nozzle. Check fill quantity again after the machine reaches its usual operating temperature.
On an integrated filling and capping line, oil on the neck can reach closure components and complicate downstream handling. Bottle rinsing, drying, conveying, and capping cannot substitute for a clean filling cutoff. Their timing does matter, though: a bottle that moves away too soon can turn an otherwise contained final drop into a spill.
For an OEM line or a small-business retrofit, confirm which adjustments the actual machine supports before specifying a solution. Independent reverse volume, speed, and timing can help with troubleshooting, but suitable nozzle design and dependable shutoff remain essential.
Save the validated recipe together with nozzle type, oil temperature range observed during testing, and supply settings. If dripping returns, compare those conditions first. When a previously clean tip starts refilling after cutoff, inspect pressure stability and valve condition before adding more suck-back.
Thank you very much for writing to us. Please leave your message and contact information, we will reply to you within 24 hours.