What Should a Complete Washing-to-Packing Line Quote Include?
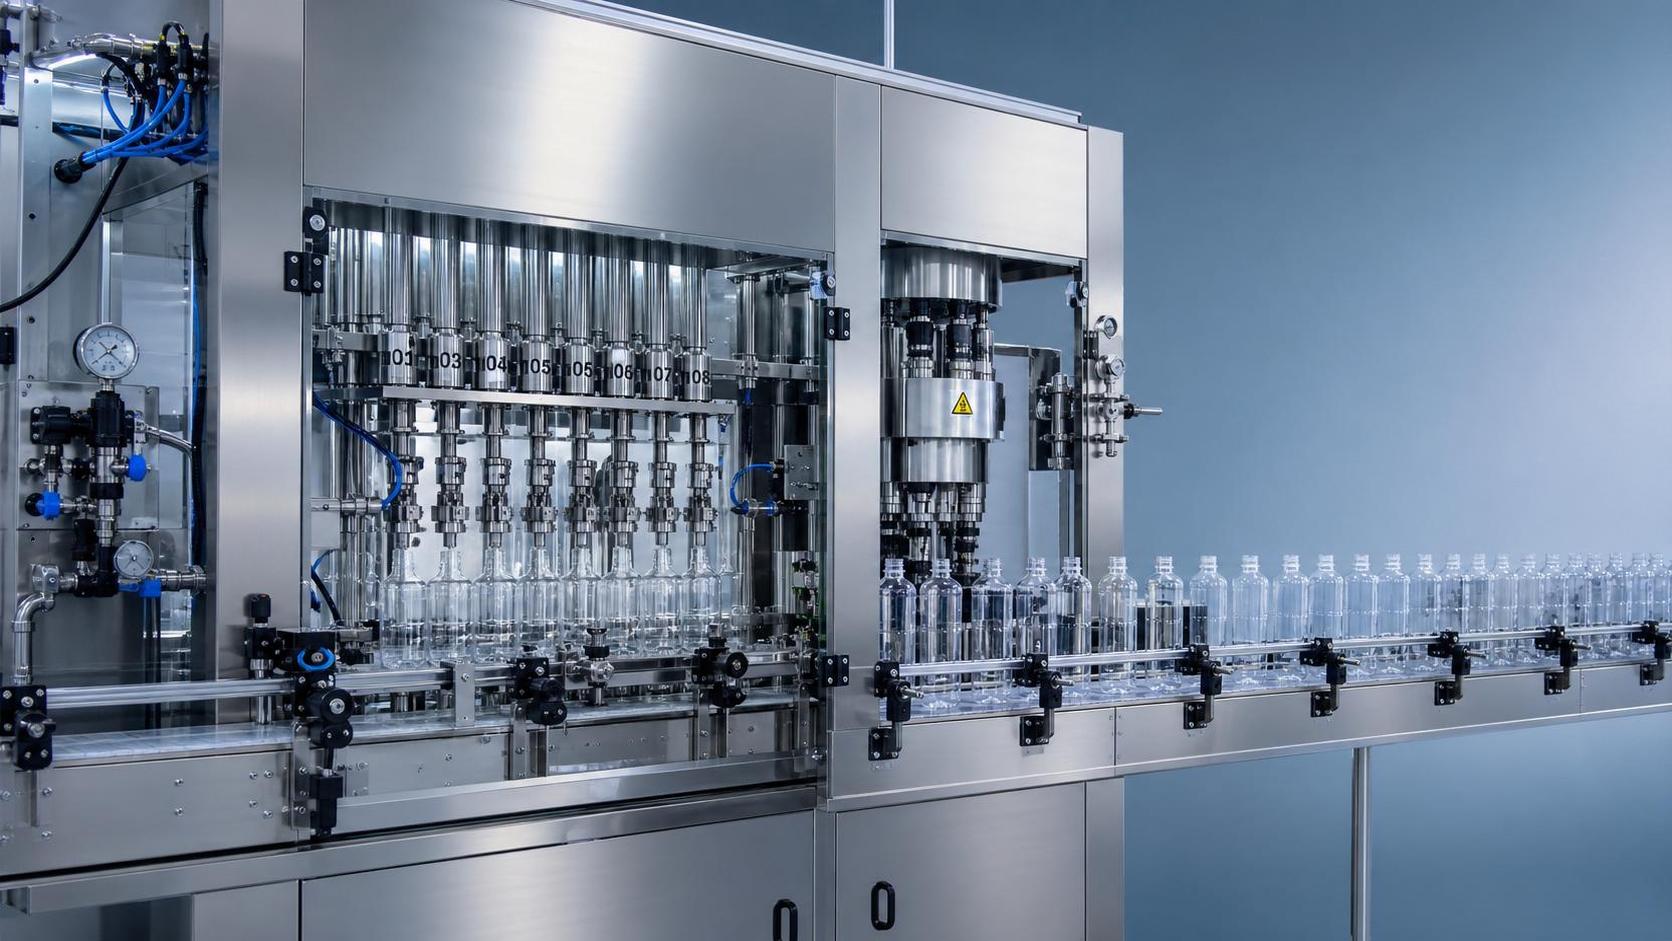
One supplier can provide washing, filling, capping, and packing equipment as an integrated line. But a single quotation does not automatically mean single-point responsibility. A complete washing-to-packing line quote must define the production result being purchased, the equipment and services required to achieve it, and who resolves problems at the interfaces between machines.
The strongest comparison is therefore not the total machine price. It is the price for an agreed operating scope: specified products and containers, acceptable finished packs per hour, defined quality limits, installed utilities, and a workable acceptance test. Without those boundaries, two apparently similar quotations may cover substantially different projects.
Define where the line starts—and where it actually ends
“Complete line” has no useful contractual meaning unless its boundaries are written down. Washing may begin with manually loaded bottles, an automatic unscrambler, or bottles arriving from a separate container-making process. Packing may end at capped bottles, shrink-wrapped multipacks, sealed cartons, or finished pallets. Each interpretation changes equipment, labor, floor space, and price.
The quote should identify every process stage and its supply status. A scope schedule can distinguish included equipment, priced options, buyer-supplied equipment, and exclusions.
Not every application needs every stage. The requirement is an explicit process boundary, not the longest equipment list. If cartons are manually erected and packed before automatic sealing, the quotation should say so rather than describe the entire packing section as automatic.
Specifications must connect the machines to the actual product
A quotation based only on “liquid filling” or “one-liter bottles” leaves too much unresolved. Filling behavior depends on viscosity, temperature, foaming, particulates, and chemical compatibility. Handling depends on bottle geometry, rigidity, neck finish, surface condition, and stability on conveyors.
The technical basis should identify the approved product and packaging range, preferably through a referenced specification matrix. Relevant inputs include:
- Product properties at the intended filling temperature, including any significant variation.
- Nominal fill volumes and the required fill tolerance, with a defined measurement method.
- Container dimensions, materials, neck finishes, and dimensional tolerances.
- Closure drawings, liner or seal details, and required application criteria.
- Label, film, carton, and pack-pattern specifications where those operations are included.
These details affect equipment selection. A foaming detergent may require a different filling sequence from a free-flowing beverage. Edible oil can create drip-control and exterior-cleanliness requirements. A lightweight bottle may need different transfer arrangements from a rigid glass container.
Washing also needs a defined purpose. Removing loose particles, rinsing with treated water, and achieving a validated microbial reduction are different requirements. The quotation should specify the medium, operating parameters, drainage arrangements, and treatment objective. A bottle rinser should not be treated as a sterilization system without an appropriately supported process specification.
For multiple formats, distinguish adjustment from conversion. Guide-rail adjustment may require no additional parts, while a neck change can require new handling components. Each quoted format should identify its change parts, settings, and any operating restrictions.
Capacity should describe saleable output, not the fastest machine
A filler’s advertised speed is not a line-performance guarantee. The completed system is constrained by its bottleneck and affected by transfers, material replenishment, stops, and rejects. A fast filler paired with insufficient cap feeding or undersized case packing does not deliver the same output at the end of the line.
The quotation should state guaranteed output for defined product-container combinations, measured as acceptable finished units at an agreed discharge point. It should distinguish instantaneous running speed from sustained output over a specified test period.
For example, a requirement for 6,000 acceptable bottles per hour is incomplete unless the bottle size, liquid, closure, packing format, test duration, and permitted interventions are also defined. Whether material replenishment, minor stops, or rejected units count against performance must be agreed before testing.
Fill accuracy needs the same discipline. “High precision” is not an acceptance criterion. The specification should define the target, permissible variation, sampling procedure, measurement conditions, and treatment of individual failures. Closure quality may require agreed torque limits, leak testing, or other criteria appropriate to the package.
If performance depends on minimum staffing, continuous product supply, or packaging materials within specified tolerances, those conditions belong beside the capacity commitment—not in an unrelated disclaimer.
Conveyors and controls determine whether the machines function as one line
Conveyors are not merely connections between machines. Their length, speed, transfer geometry, and accumulation capacity affect how disturbances move through the system. Insufficient buffering can cause a short downstream stop to interrupt filling immediately; unsuitable transfers can destabilize containers or damage packaging.
The quotation should reference a layout showing machine positions, conveyor routes, working heights, access space, and material-loading points. It should also identify the assumptions behind the layout, including building dimensions, columns, drains, and available maintenance clearance.
Controls integration deserves its own scope description. It should establish:
- How upstream equipment responds when downstream equipment stops or becomes blocked.
- How container presence, cap shortages, rejects, and product shortages are detected and handled.
- Which machine or line controller coordinates operating states and alarms.
- How emergency stops, guarding, and restart behavior are coordinated across equipment boundaries.
- What software backups, access credentials, drawings, and licenses are handed over.
When several manufacturers contribute machines, name the party responsible for interface design and line-level troubleshooting. A supplier may subcontract equipment and still provide effective integration, but responsibility for the combined result must remain clear. Otherwise, each machine can meet its individual specification while the complete line fails its output requirement.
Utilities, hygiene, and site work belong in the priced scope
A utility schedule should provide more than connected electrical power. It should identify required voltage and frequency, operating demand, compressed-air pressure and consumption, water quality and flow, drainage, and any steam, cooling, extraction, or ventilation requirements. Peak demand should be distinguished from average consumption where that difference affects infrastructure sizing.
The supply boundary matters equally. A machine may include an air preparation unit but exclude the compressor and distribution piping. A rinser may include spray nozzles but exclude water treatment. A heated shrink tunnel may require electrical capacity or ventilation work outside the equipment package.
Cleaning provisions should match the product and operating regime. If clean-in-place capability is offered, specify which circuits are covered, how cleaning media circulate and drain, which components still require removal, and whether the cleaning skid is included. “Easy to clean” does not establish cleaning effectiveness or define the labor involved.
Materials should be specified by service conditions rather than by a generic stainless-steel claim. Product-contact metals, seals, hoses, and plastics need compatibility with the product and cleaning chemicals. Food, pharmaceutical, and chemical applications impose different documentation and validation needs; a general-purpose machine description cannot establish suitability for all three.
The quote should identify applicable destination-market requirements and the documents included to support them. Component certificates alone do not establish conformity of the assembled line.
Acceptance testing turns specifications into enforceable commitments
Factory acceptance testing and site acceptance testing answer different questions. Factory testing can verify construction, controls, handling, and agreed performance under available conditions. Site testing confirms operation after transport, installation, and connection to the actual utilities and upstream or downstream systems.
The quotation should reference an acceptance protocol, or at least define the contractual basis for one. It needs to state the products and packaging formats tested, trial duration, sampling methods, quality limits, output criteria, and required records.
Test materials are a meaningful cost and scheduling issue. Specify who supplies bottles, caps, labels, cartons, and product; the quantities required; delivery deadlines; and disposal arrangements. Where substitute liquids are used, record which characteristics they reproduce and which performance claims still require confirmation with the actual product.
Acceptance also needs a failure procedure: who corrects deficiencies, who pays for retesting, and what happens when site readiness prevents a valid test. Payment milestones should reflect verifiable events. Shipment readiness, mechanical installation, successful commissioning, and final acceptance are not interchangeable achievements.
Installation, support, and commercial terms can change the real project price
“Installation included” may mean supervision rather than a fully staffed installation service. The quotation should allocate unloading, rigging, positioning, anchoring, utility connections, conveyor assembly, commissioning, and waste removal. Travel, accommodation, visas, local transport, and overtime should have an explicit pricing basis.
Training should specify its duration, language, scope, and deliverables. Operation, format changeover, cleaning, preventive maintenance, and fault diagnosis require different instruction. The documentation package should include operating manuals, electrical and pneumatic drawings, spare-parts lists, maintenance schedules, and relevant calibration or inspection records.
After-sales terms need practical detail: warranty start point, coverage, exclusions, remote-support arrangements, on-site service charges, and spare-parts availability. Distinguish response time from repair time. A promise to answer a service request does not guarantee that production can restart within that period.
Commercial clarity requires a named delivery term and place, packaging arrangements, freight and insurance allocation, payment currency, quotation validity, and responsibility for import-related costs. Delivery timing should identify its trigger, such as deposit receipt, drawing approval, or arrival of sample containers.
Any provisional item should carry an allowance or a clear pricing mechanism. Leaving electrical modifications, additional conveyors, change parts, or commissioning days unpriced does not remove those costs; it postpones the negotiation until the project has less flexibility.
Compare the cost of reaching the same operating result
Before comparing totals, align the proposals against one agreed specification. Record whether each requirement is included, optional, excluded, or dependent on an assumption. A short exclusion list is not necessarily better than a detailed one: transparent exclusions make it possible to calculate the actual project cost.
The comparison should include equipment, integration, required options, site preparation, delivery, installation, testing, training, and initial spares. Recurring differences—such as operator requirements, cleaning labor, utilities, and format-change costs—should be evaluated separately rather than hidden inside a speculative payback claim.
The decisive question is whether the quotation connects scope, performance, responsibility, and acceptance. If a required production outcome cannot be traced to an included item, an assigned obligation, and a testable criterion, the proposal still contains an unresolved project risk. Resolving that gap before ordering is more valuable than negotiating a discount on an incomplete line.
Thank you very much for writing to us. Please leave your message and contact information, we will reply to you within 24 hours.