When Is a Partial Retest Enough for an Installed Lubricant Filler?
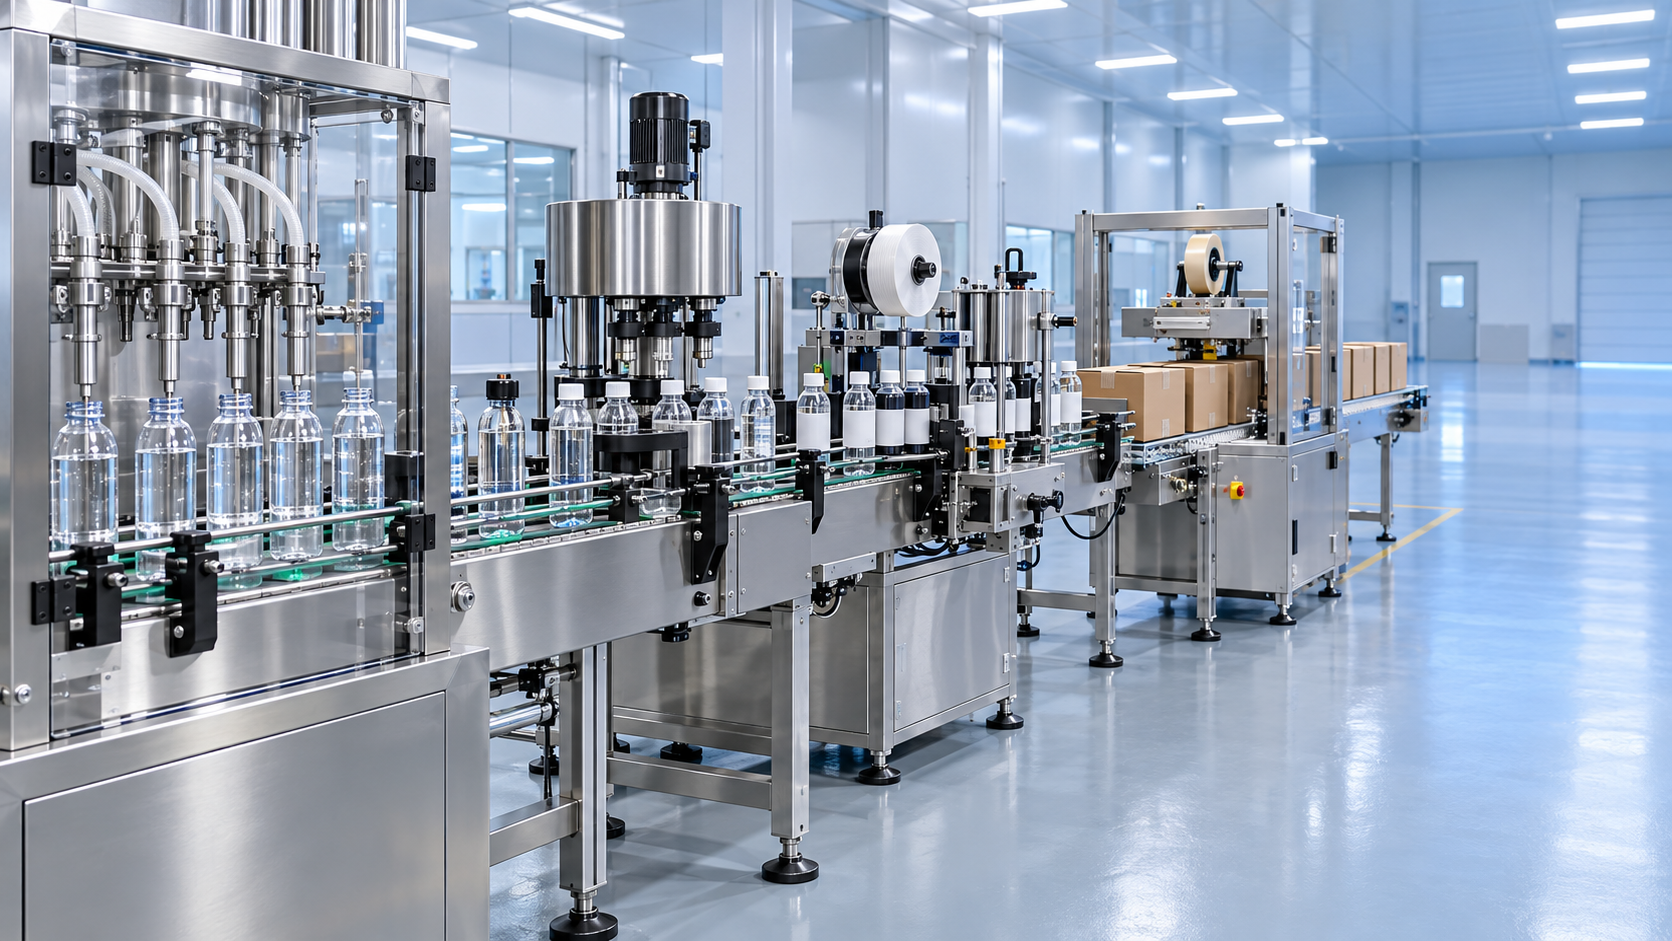
A lubricant filler may start a run on target, then gradually produce lighter or heavier bottles. After a nozzle repair or pressure adjustment, the immediate question is whether production can restart after a focused check. A partial retest is justified when the cause is established, the correction has a bounded effect, and documented testing can confirm the affected functions without leaving credible risks untested. A few acceptable bottles after adjustment are not enough.
For an installed machine, the decision also depends on its approved baseline and site change-control requirements. Replacing one worn component may support targeted testing; changing shared pressure control, filling logic, or the operating range usually requires broader verification. The distinction matters because an unnecessarily wide test delays production, while an overly narrow one can miss continuing underfill, excess giveaway, or unstable performance.
What does a partial retest need to prove?
A partial retest repeats selected checks from an established acceptance or qualification program. It does not replace the original program or assume that unchanged equipment is automatically unaffected. Its purpose is to show that the corrected function works and that relevant interfaces still perform as intended.
A defensible scope answers three questions:
- What failed? Identify the affected component, operating condition, or measurement process, with evidence supporting the diagnosis.
- What could the correction influence? Trace effects through the product supply, filling heads, controls, measurement system, and connected line equipment.
- What evidence remains valid? Explain why previous results still support functions excluded from the retest.
For example, replacing an identical seal in one independently controlled filling head may leave bottle handling and recipe management unchanged. Even then, the test should address leakage, fill repeatability, cutoff behavior, and any disturbance caused during maintenance. The physical size of a repair does not define its testing boundary.
Why does lubricant fill weight drift during a production run?
Temperature-driven viscosity changes, unstable supply pressure, trapped air, nozzle wear, and measurement errors can all contribute. Distinguishing them matters because the same symptom can require very different retest scopes.
Temperature and filling principle
As lubricant warms, viscosity commonly decreases, changing flow resistance, valve response, and drainage after cutoff. On a time-pressure filler, these changes can alter the quantity delivered during a fixed opening time. A volumetric filler may deliver a consistent volume while net mass changes with density. For a mass-based filler, density alone should not shift the mass target, but changing flow behavior can affect cutoff overshoot.
Record product temperature at a representative point near filling, not only room temperature. Compare the drift with warm-up, recirculation, and tank replenishment. A correction verified only with cold product does not demonstrate control over a problem that appears after thermal stabilization.
Supply conditions and individual heads
A falling supply level, pump pulsation, restricted filter, unstable regulator, or air ingress can change delivery. Foam or entrained air can also make immediate weight readings unstable. When all heads move together, investigate shared conditions before changing individual head settings.
One consistently abnormal head points more strongly toward local valve wear, seal leakage, nozzle buildup, or calibration differences. This is a diagnostic clue, not proof: shared supply disturbances may affect heads differently because their flow paths differ.
The weighing process itself
Apparent drift may come from changing bottle tare weights, an unstable scale, vibration, drafts, or inconsistent handling of dripping bottles. Confirm balance suitability and calibration status before adjusting the filler. Use individual tare measurements when packaging variation is significant relative to the allowed fill-weight variation.
If the reference measurement is unreliable, the retest cannot establish machine performance. Correcting the measuring system may also require reviewing earlier production decisions, rather than merely repeating a machine check.
Which changes can reasonably support a targeted retest?
The following situations can support partial testing, provided the diagnosis and impact assessment justify the exclusions. They are not automatic exemptions from broader testing.
“Like-for-like” should mean equivalent relevant specifications, not simply that the replacement fits. Nozzle bore, valve response, seal compatibility, sensor range, and component configuration can change performance even when installation is straightforward.
A change affecting several heads does not necessarily demand repetition of every original installation test. It does, however, weaken the argument for testing only one head. The scope should follow the affected function and its dependencies, rather than defaulting to either a single bottle check or complete requalification.
What should the retest plan include before production restarts?
Write the acceptance criteria and sampling rationale before collecting results. Otherwise, there is a risk of stopping the test as soon as the numbers look favorable.
- Establish the reference condition. Record the lubricant grade, container, recipe, target quantity, line speed, active heads, supply conditions, and relevant temperature range. Identify the earlier approved results used for comparison.
- Confirm the correction. Record the fault evidence, work performed, parts or settings changed, and checks that verify correct installation or configuration.
- Challenge the suspected failure mechanism. Include the conditions under which the problem appeared, such as warm operation, declining tank level, replenishment, or restart after a pause.
- Measure both location and time. Keep individual results by head and sampling point. Evaluate average fill, variation, and any continuing trend rather than relying on a pooled average.
- Define release and escalation rules. State which results permit release, which require investigation, and which trigger wider testing.
There is no universal sample count or test duration suitable for every installed lubricant filler. The plan should reflect process variability, defect risk, the number of heads, previous evidence, and applicable site or customer requirements. A drift problem requires observations over a relevant operating period; a short repeatability test cannot substitute for that.
Acceptance limits should come from the approved product and process specifications, including applicable quantity requirements. Avoid inventing a convenient percentage after the repair. Individual-container limits, average quantity, and process stability may represent separate acceptance questions.
Is testing only the repaired head enough?
Sometimes, but only where the head is sufficiently independent and the work has not disturbed shared systems. A localized nozzle intervention may justify detailed testing of the repaired head with a smaller comparative check across unaffected heads.
That argument becomes weaker when heads share a pump, manifold, pressure regulator, timing reference, or control parameter. Repairing one valve can alter shared flow demand. Likewise, changing a common cutoff setting to compensate for one worn head can shift every head away from its previous condition.
Test at representative production demand, not only with one head operating slowly. Simultaneous filling may reveal pressure loss or interaction that isolated operation hides. Where conveyor motion or container positioning affects nozzle alignment, relevant checks should also run with normal line movement.
When should the scope expand beyond a partial retest?
Expand testing when the cause remains uncertain or the change invalidates assumptions behind the existing acceptance evidence. This does not always mean repeating every historical check, but it does require a broader, documented assessment.
Typical triggers include:
- Changing the filling principle, metering arrangement, pump type, or nozzle geometry.
- Modifying software, weighing algorithms, shared timing, or control logic that can affect multiple functions.
- Operating outside the previously demonstrated range for product viscosity, temperature, container format, or speed.
- Recurring drift after apparently successful corrections, especially across several heads.
- Loss of traceable baseline records or uncertainty over earlier undocumented adjustments.
- Unexpected leakage, pressure excursions, or changes to guards, interlocks, or other safety-related functions.
A new lubricant grade deserves particular scrutiny. Similar nominal viscosity does not establish equivalent behavior: density, air release, foaming, and temperature response can differ. A targeted product trial may be appropriate, but previous evidence should not be transferred solely because both products are lubricants.
Where machine-specific dependencies are unclear, obtain the relevant control documentation or technical input before approving exclusions. Safety-related changes require their own verification; acceptable fill weights do not prove that protective functions remain effective.
What records are needed to release the filler?
The release record should connect the original symptom to the diagnosis, correction, test scope, raw results, and approval. Include measurement equipment identification, test conditions, head-level data, deviations, and the reason excluded functions remain covered by existing evidence.
Any adjustment made during testing must be recorded. Results collected before and after a setting change should not be merged as though they represent one stable process. Repeated tuning until samples pass is troubleshooting, not a completed retest; the final configuration still needs its planned verification.
Equipment release and product disposition are separate decisions. Passing a retest does not establish that bottles produced before the fault was detected are acceptable. Define the potentially affected production interval using available records and assess that product under the site's hold, inspection, or disposition procedure.
Can production resume with extra weight checks?
Enhanced monitoring can support restart after the defined acceptance criteria have been met, particularly when confirming continued stability over subsequent production. It should specify sampling locations, temperature or supply observations, action limits, and who must respond to a deteriorating trend.
Extra checks are not a substitute for resolving an unexplained failure. If acceptable weight depends on repeated operator compensation, or drift returns under the same conditions, the correction has not demonstrated stable control. Keep the affected operation restricted and reopen the investigation rather than extending a partial-retest justification beyond its evidence.
Thank you very much for writing to us. Please leave your message and contact information, we will reply to you within 24 hours.